Chinese
 English
 français
 Deutsch
 italiano
 español
 português
 日本語
 한국의


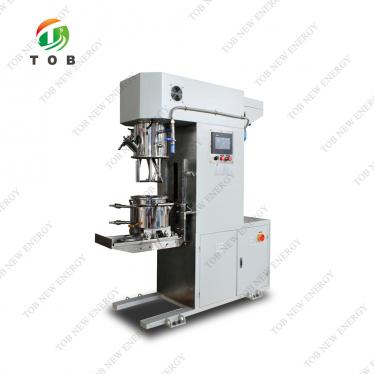
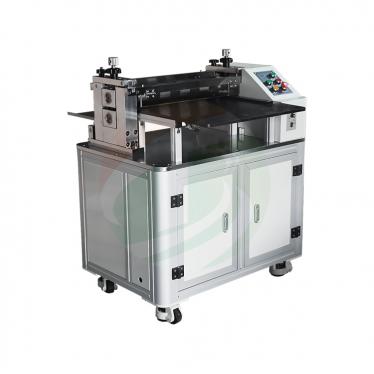
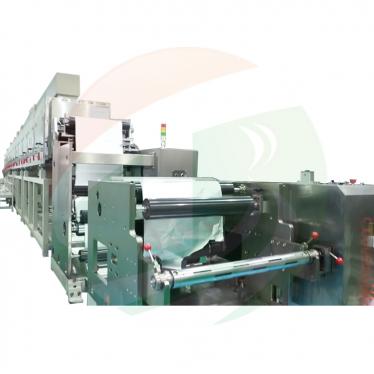
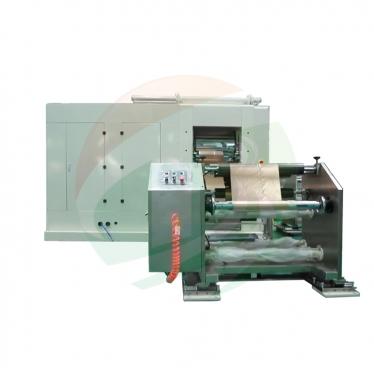
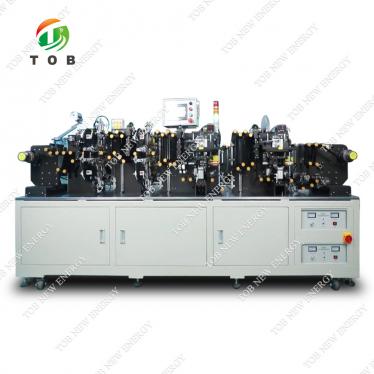
Project case study · Europe · 2026
An integrated 32140 tabless cylindrical cell line engineered around a stainless-steel enclosure.
TOB NEW ENERGY coordinated electrode processing, tabless jelly-roll assembly, collector joining, can assembly, electrolyte filling, formation and sorting as one production system.
- Project year
- Location
- Europe
- Cell format
- 32140 cylindrical cell
- Architecture
- Tabless current collection
- Enclosure
- Stainless-steel can
- Service scope
- Engineering, delivery, installation, commissioning and technical support
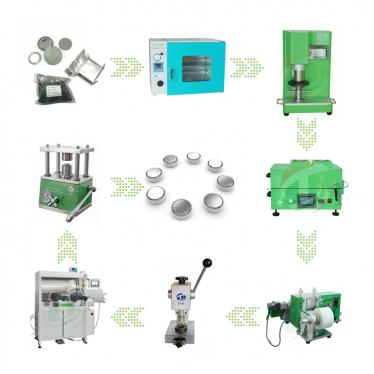
Project image(assembly process) gallery · 13 imagesUse the arrows or swipe left and right to follow the 32140 cell assembly process.
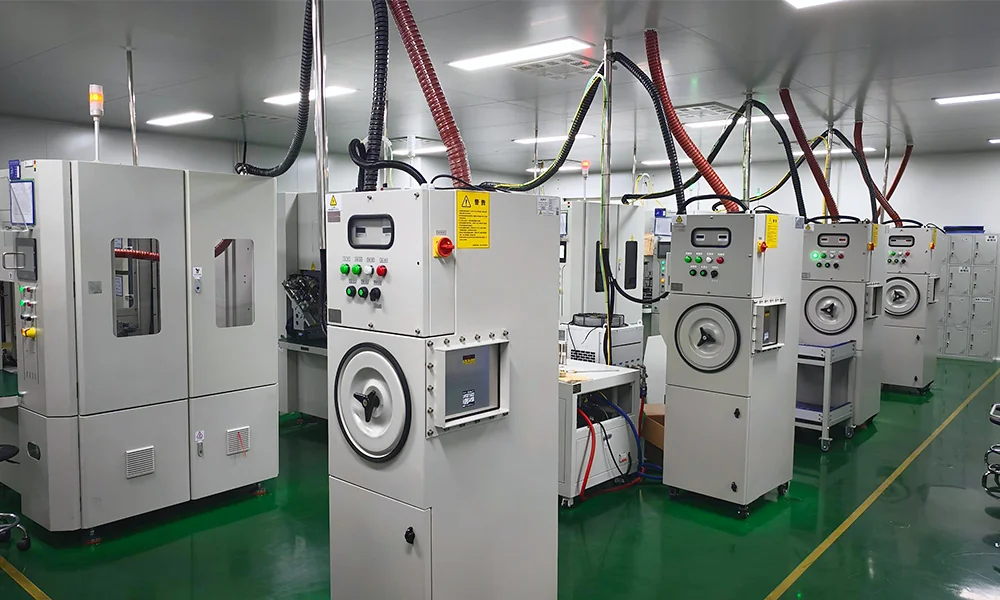
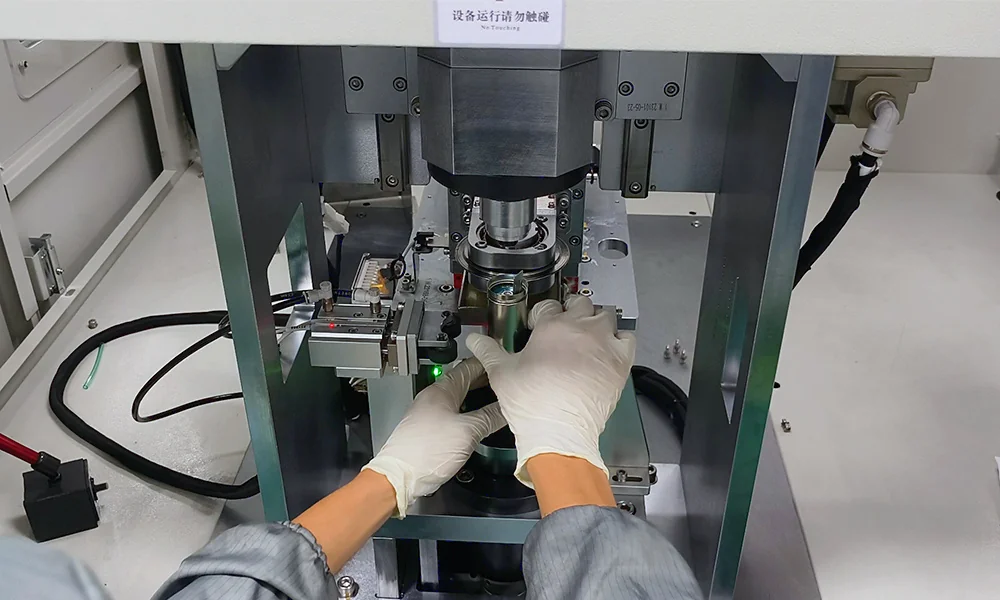
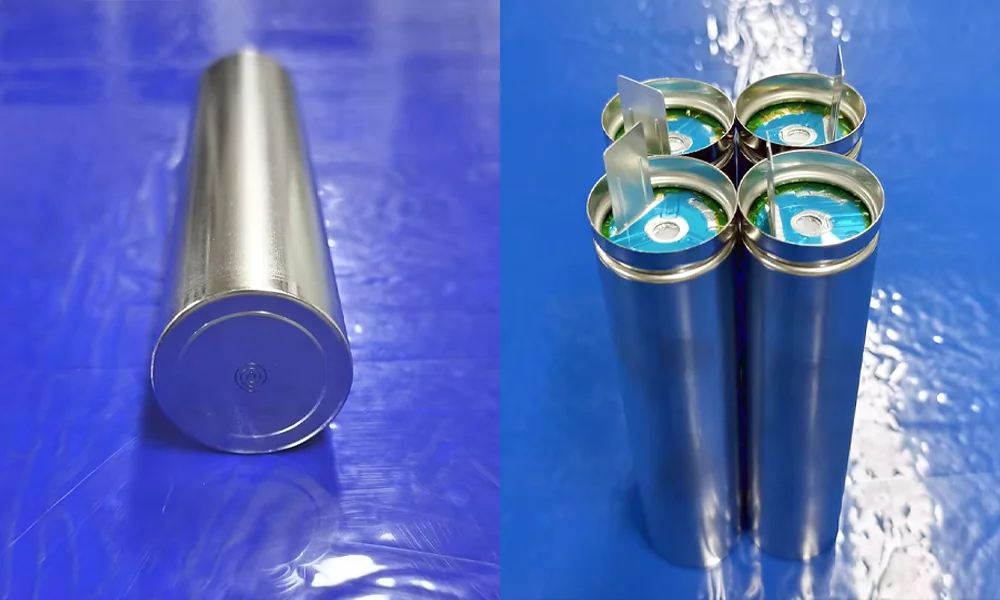
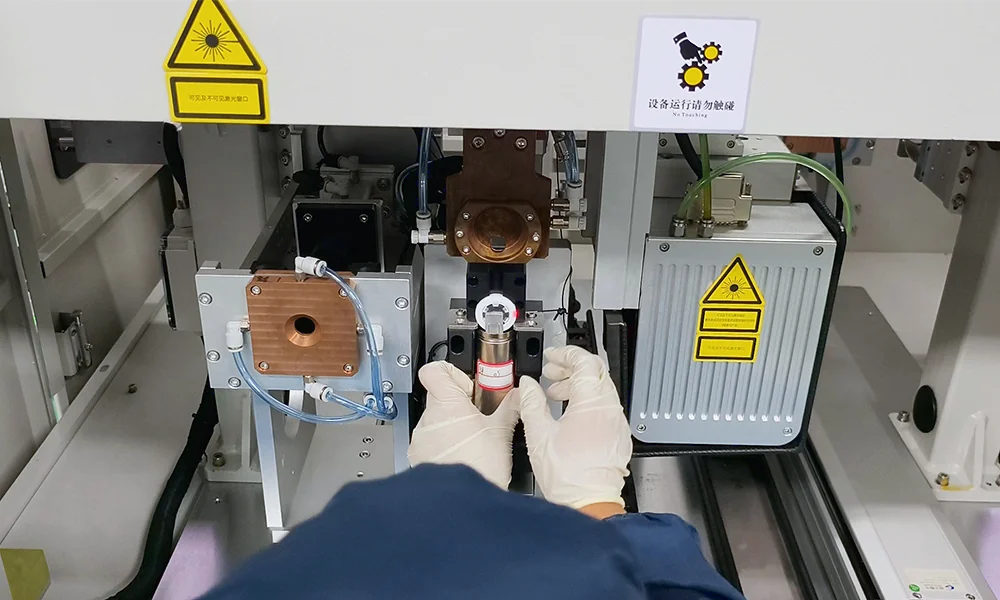
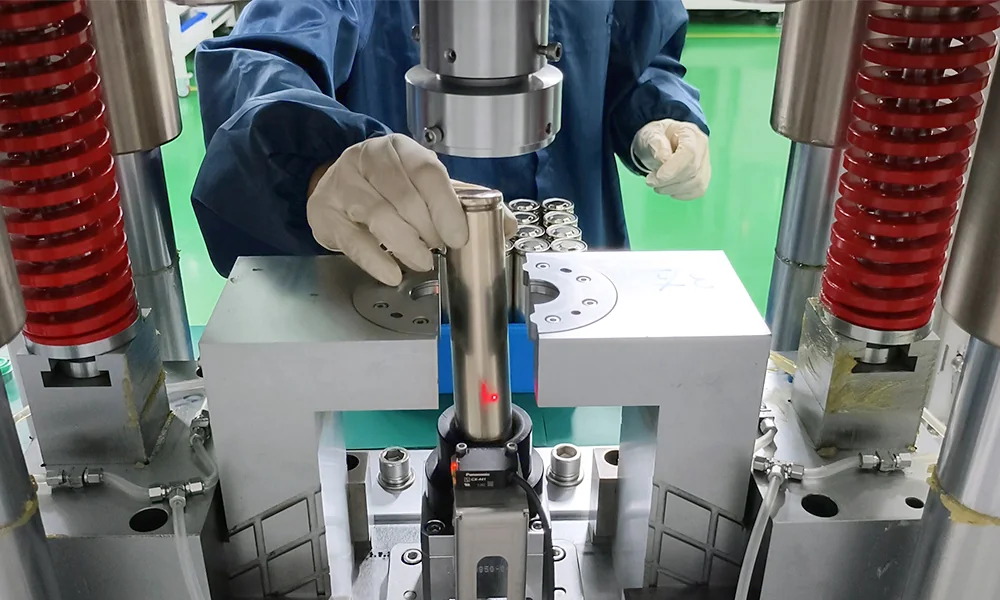
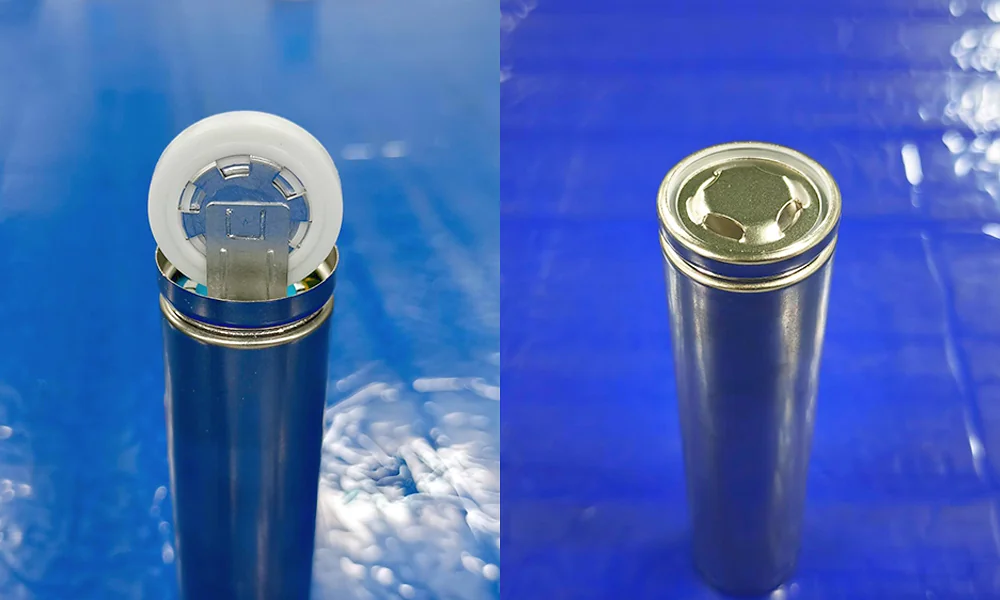
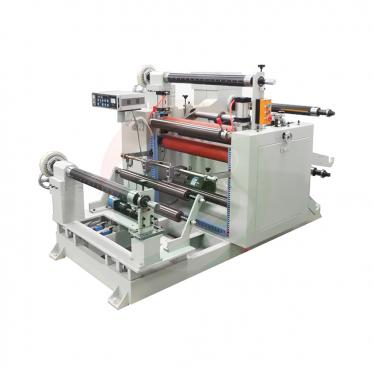
Electrode Processing
Mixing, coating, calendering, slitting and high-vacuum roll drying.
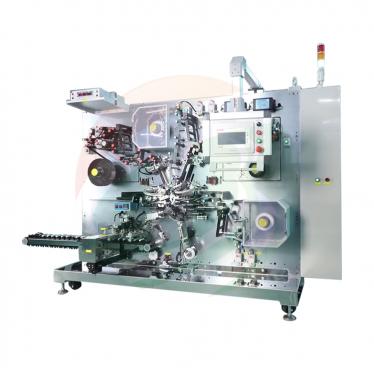
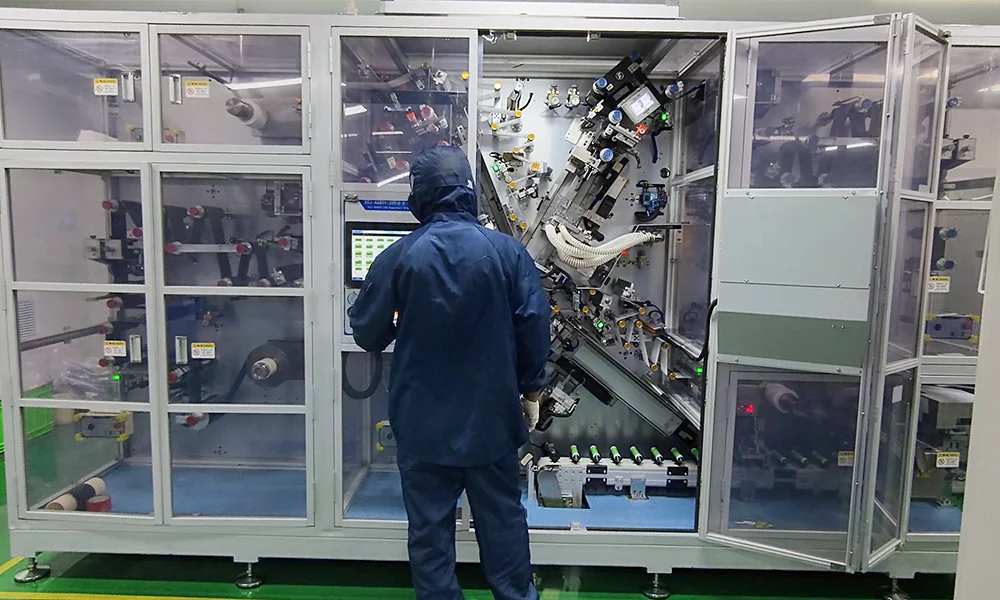
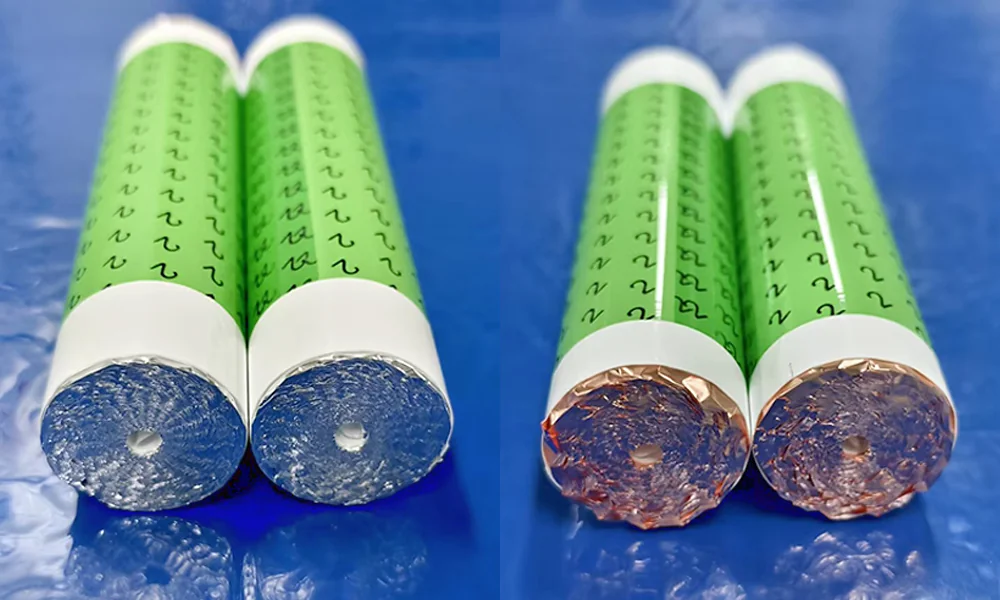
Tabless Winding
Controlled tension and alignment establish the 32140 jelly-roll geometry.
End Forming
Exposed foil edges are formed into stable collector-contact surfaces.
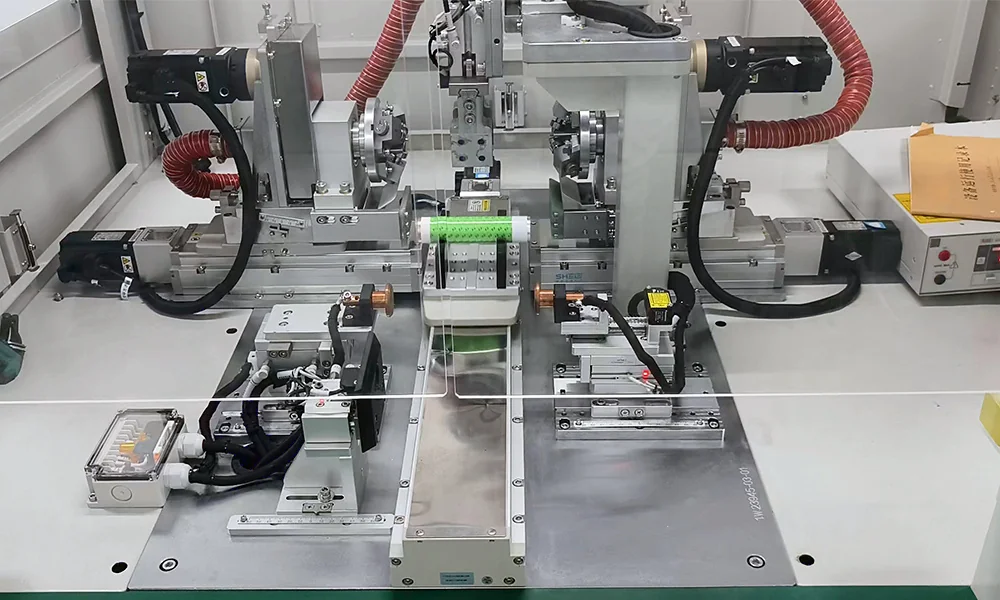
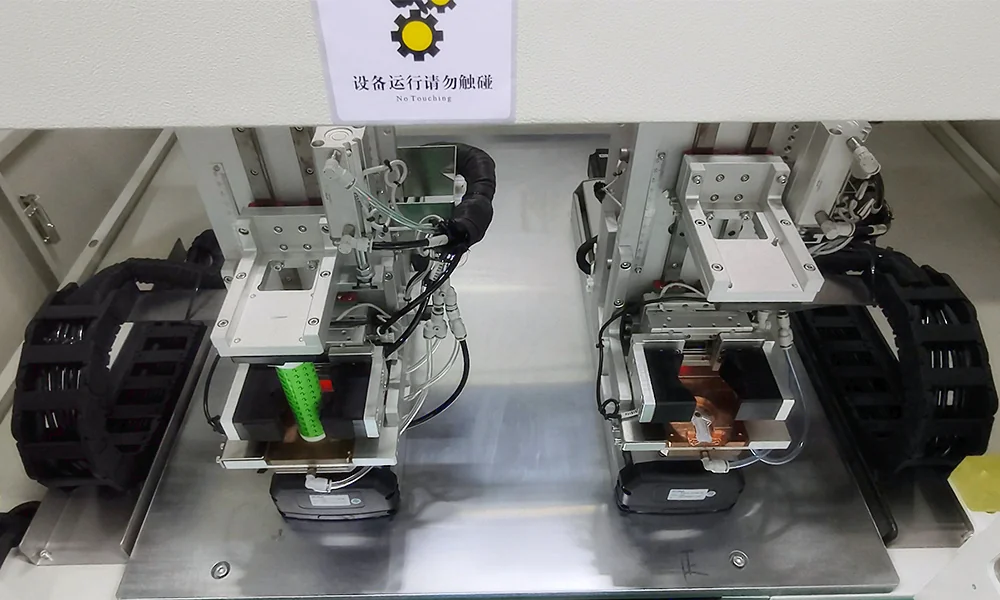
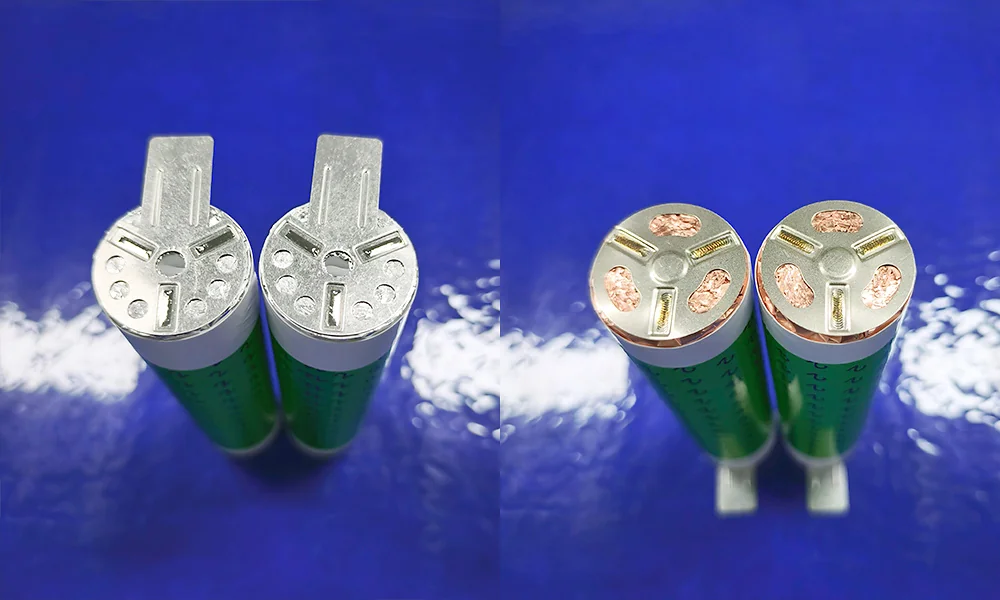
Collector Joining
Collector discs are positioned and laser-welded using the approved process window.
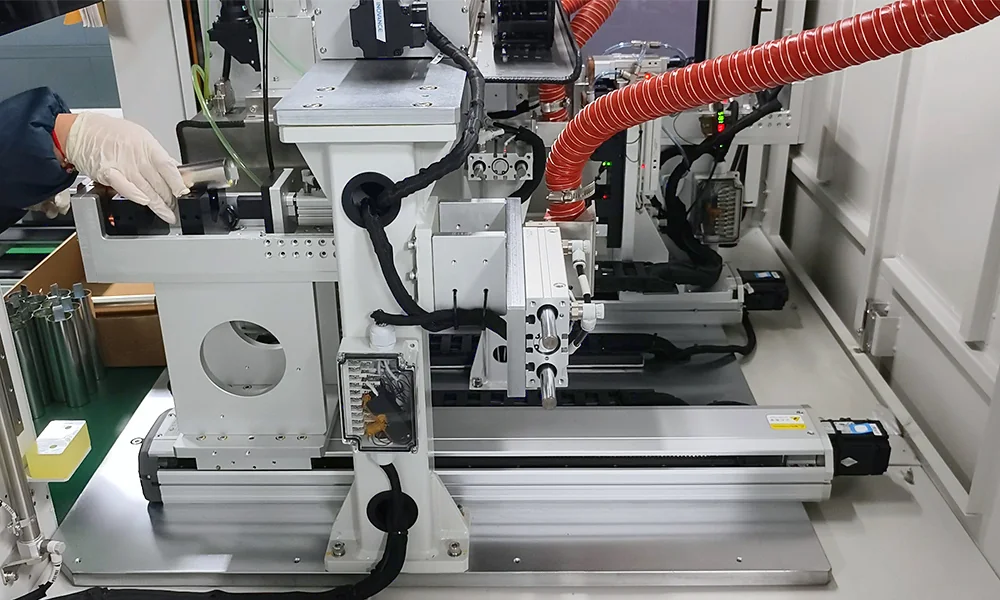
Can Assembly
Insulation, stainless-steel can insertion, grooving, filling and sealing are coordinated.
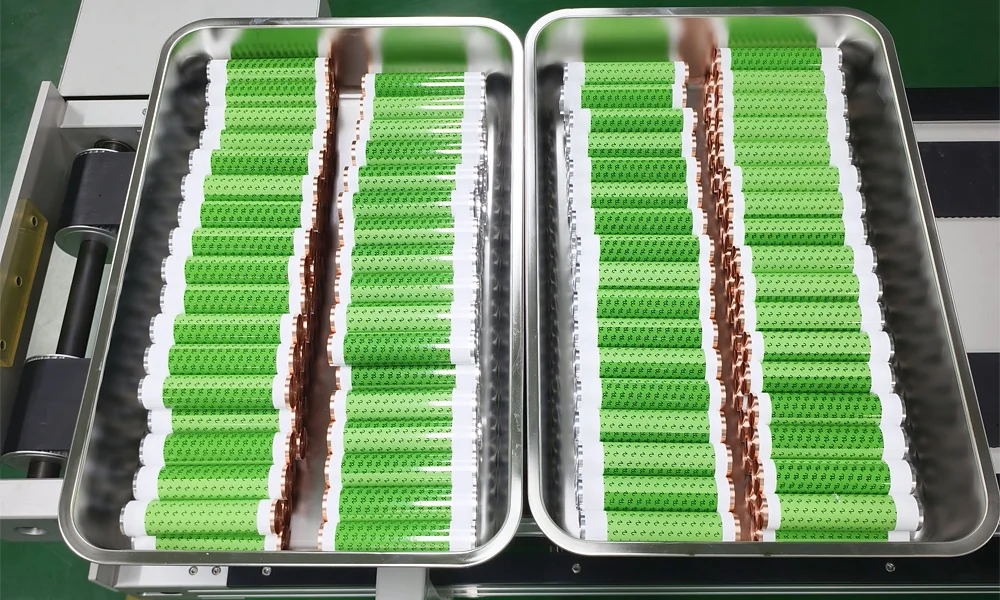
Formation & Sorting
Formation, aging, testing, grading and sorting retain the required quality records.
32140
Cell format
A large-format cylindrical-cell manufacturing route.
Tabless
Current collection
Continuous foil-edge contact coordinated with end forming and welding.
Steel
Cell enclosure
Stainless-steel can assembly with matched insulation and sealing steps.
End-to-end
Delivery scope
Engineering through installation, commissioning and technical support.
Customer Priorities & Engineering Response
The project was defined around the relationships between electrode-edge geometry, long-format winding, distributed current collection and traceable back-end testing.
Prepare Consistent Electrode Edges
TOB engineering responseLinked slurry preparation, coating, calendering, slitting and vacuum drying with the exposed-foil geometry required by the tabless structure.
Control the Long Jelly Roll
TOB engineering responseSpecified controlled tension, web guidance and alignment so the cathode, separator and anode form uniform end faces after winding.
Join Collectors Repeatably
TOB engineering responseCoordinated end-face forming, collector positioning, laser-welding parameters and electrical inspection as one connected process.
Retain Traceable Cell Data
TOB engineering responseConnected formation, aging, testing, grading and sorting records to the customer's approved classification and lot-management requirements.
Production Line Design Basis
Final machine settings and acceptance criteria are defined against the customer-approved cell drawing, materials, process recipe, target output and factory conditions.
| Cell format | 32140 cylindrical battery cell |
|---|---|
| Cell architecture | Tabless / continuous current collection |
| Cell enclosure | Stainless-steel can |
| Front-end scope | Slurry preparation, coating, calendering, slitting and high-vacuum electrode-roll drying |
| Assembly scope | Winding, jelly-roll end forming, collector-disc joining, can assembly, grooving, filling and sealing |
| Back-end scope | Formation, aging, electrical testing, capacity grading and automatic sorting |
| Project services | Engineering, equipment delivery, installation, commissioning and technical support |
| Final configuration | Matched to the approved cell design, material system, quality plan, output and automation level; review a related tabless cylindrical battery production line for an example of TOB's integrated line scope. |
Swipe horizontally to review the full design-basis table.
Core Equipment & Process Controls
The equipment groups cover the route from prepared battery materials to graded 32140 cells. Final parameters remain subject to the approved technical specification.
Project Value & Delivery
A Controlled Route from Electrode Processing to Graded 32140 Cells
TOB NEW ENERGY coordinated equipment interfaces, process handoffs, quality-control points and technical support around the customer's approved 32140 cell design and factory conditions. The platform provides a structured basis for recipe refinement, engineering review and future capacity planning.
Project facts are based on the 2026 TOB NEW ENERGY project brief. Final performance figures and acceptance criteria remain specific to the customer's validated materials, product specification and project records.
Electrode preparation and moisture-control operations are linked to tabless assembly requirements.
Winding, end forming, collector joining and stainless-steel can processes are coordinated.
Formation, aging, testing, grading and sorting support traceable classification.
Installation, commissioning, training and technical support form part of the project scope.
Planning a 32140 tabless cylindrical cell project?
Provide the target cell drawing, chemistry, annual output, process scope, automation level and workshop conditions so the engineering team can review the production route and critical interfaces.
 Abonneer u op ons